❌

Reading view

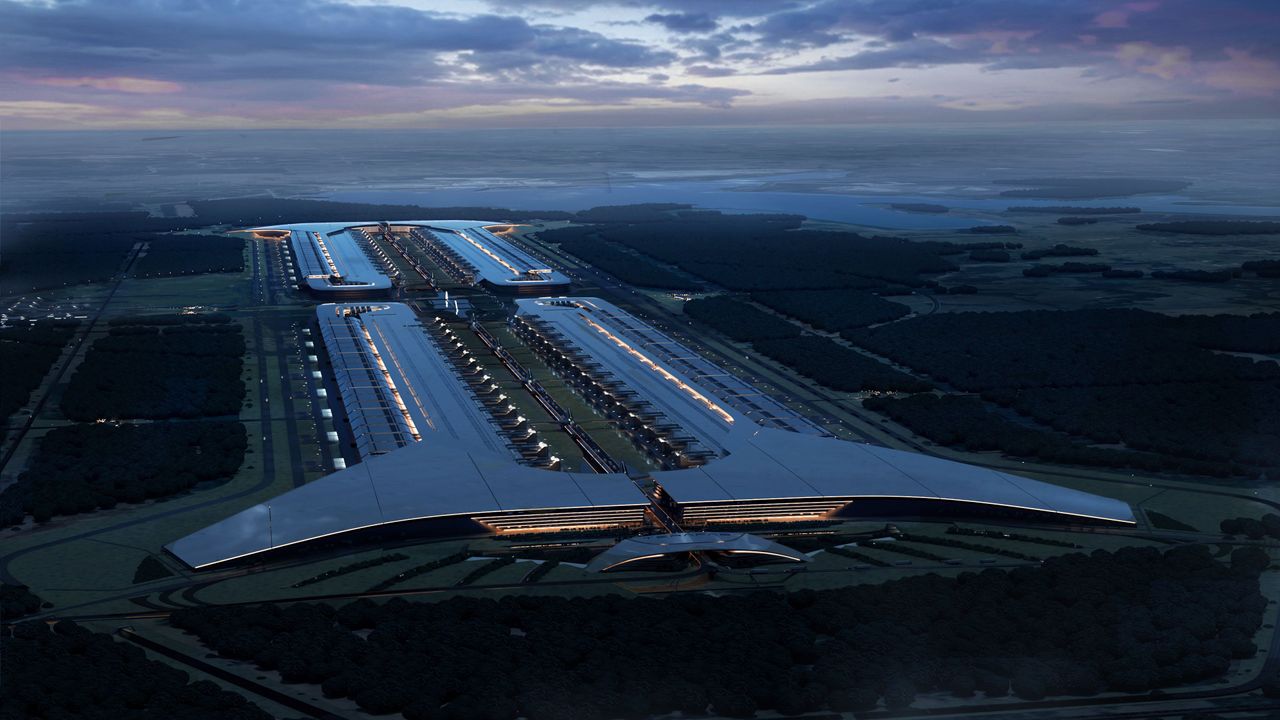
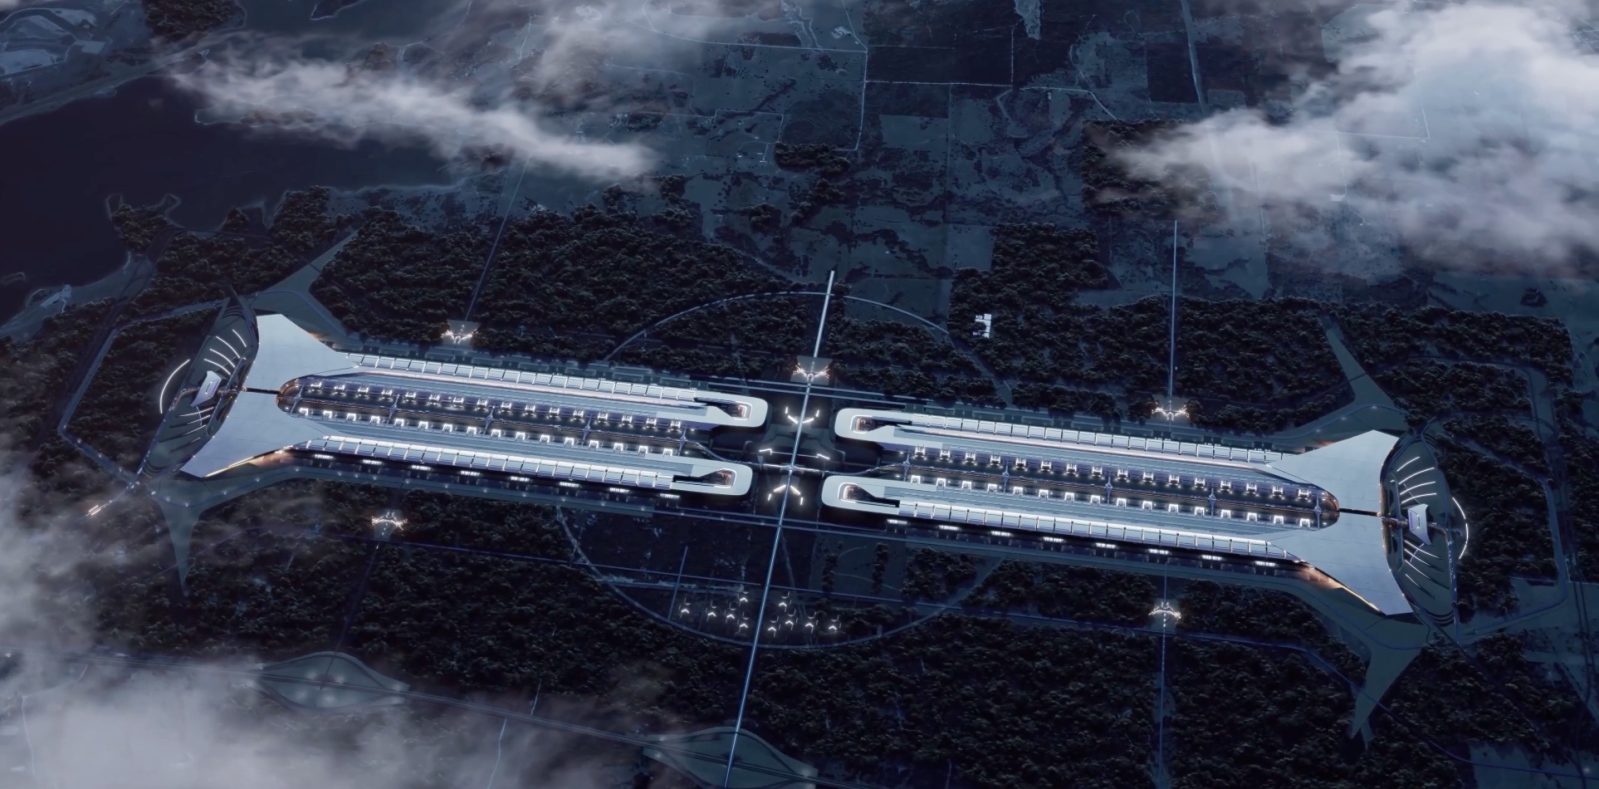
Musk’s Terafab projected to be larger than the Pentagon, Apple Park, Mall of America, and Giga Texas, combined — all-in-one chip manufacturing facility visualized to show the project’s massive footprint

Most megafactories usually take years to go from conceptualization to construction, but a recent drone flyover of the Terafab showed that progress has already started on the ground less than five months after Musk unveiled it. However, the video doesn’t do justice to the true scale of its footprint, so X user Nic Cruz Patane created a visualization to help us understand how large the chip manufacturing facility is.

Terafab approximate size comparison between Giga Texas, the Pentagon, Apple Park, and the Mall of America.There has never been a building this large. Elon Musk says it will be the most valuable building by far. pic.twitter.com/GCmpfeduJnAugust 6, 2026

The site will reportedly have a floor space of at least 100 million square feet, making it larger than Giga Texas (10 million sq. ft), the Pentagon (6.6 million sq. ft), Apple Park (2.82 million sq. ft), and the Mall of America (5.6 million sq. ft), combined. This also makes it significantly larger than New Century Global Center in Chengdu, China, with has an interior space of “just” 18.9 million sq. ft.

While this might seem like an absurd amount of space for chip manufacturing, it appears that the Terafab will need it because it’s going to be more than just a chip fab making AI processors — instead, it will be an all-in-one facility that will produce logic and memory chips, as well as have lithography, packaging, and testing under one roof.

Elon Musk started talking about building his own chip manufacturing facility in late 2025 and officially announced the project in March of this year. The reasoning behind this project is that both SpaceX and Tesla will require at least 1TW of compute, which is more than ten times that current global chip supply.

Nvidia CEO Jensen Huang warned that a project like this will be an “extremely hard” challenge, but it appears that Musk is willing to put his massive resources on the line for this. Intel CEO Lip-Bu Tan even said that he can “think of no better partner than Elon Musk” to explore “unconventional” ways of chip manufacturing.

Musk is no stranger to both leading and funding projects that otherwise seemed impossible. Although he did not found Tesla, his investment and leadership in the company led it to become an industry trailblazer in EVs. He fundamentally changed commercial space travel with SpaceX; something that used to be the purview of NASA and other national governments, and he also broke a record when he set up 100,000 Nvidia H200 GPUs in just 19 days back in 2024 — a process which Huang said usually takes four years.

It seems that Terafab is Musk’s biggest project to date, which is estimated to require up to $119 billion in investments. But even though it seems that this project already has a secure customer base in SpaceX and Tesla, the former acknowledges that there’s a risk that this ambitious megafactory may not be successful.

  •  

Elon Musk's massive Terafab chip-making facility starts to take shape — 100 million square feet of manufacturing space and $16.8B initial capital investment

SpaceX and Tesla on Thursday formally unveiled plans for the initial phase of their Terafab project. The first stage of the plan — which is expected to use Intel's 14A process technology — is expected to require $16.8 billion in investment, while the completed campus is planned to encompass more than 100 million square feet of manufacturing space. The massive semiconductor manufacturing complex will be built in Grimes County, Texas, at a location that belongs to SpaceX.

According to SpaceX and Tesla, their combined demand for semiconductors is projected to exceed 1 terawatt (TW) of compute per year, which significantly exceeds today's global supply. In fact, SpaceX, Tesla, and xAI already consume a significant portion of contract chipmaking services available today, and can potentially justify building a dedicated fab that will exclusively serve Elon Musk's companies. In particular, Terafab is envisioned to exclusively produce AI inference processors for Tesla Optimus humanoid robots and Cybercab autonomous vehicles, as well as 'high-power' processors intended for SpaceX's space-based data centers. Meanwhile, SpaceX and Tesla have not disclosed when their combined demand for compute per year will hit the 1 TW benchmark.

Unlike a conventional semiconductor fab, Terafab is envisioned as a vertically integrated manufacturing campus where advanced logic devices, memory chips, packaging, and testing operations are housed together. Normally, logic and memory are produced at different fabs using different process technologies, whereas packaging and testing services are performed at different facilities. However, the companies believe that consolidating logic, memory, packaging, and testing in one location will not only shorten the production cycle but will also shorten time-to-yield by enabling faster iterative improvements.

Given the description and the goal of the project, this will be a massive facility. Yet, SpaceX and Tesla have said little about its capabilities; The only thing they have disclosed is that the current facility in Grimes County will feature '100 million square feet of manufacturing space.' The 100 million square feet (9.3 million square meters) figure immediately stands out because it is far beyond anything ever announced for a semiconductor manufacturing facility. For example, the total area of Samsung's Pyeongtaek campus is approximately 2.89 million square meters, or 31.1 million square feet. A single Samsung fab occupies about 120,000 square meters, or 1.29 million square feet. However, the key wording is important: '100 million square feet of manufacturing space' does not mean 100 million square feet of cleanroom space.

Based on an image published by SpaceX, the Terafab facility will occupy four massive buildings. It is unclear whether these buildings will be four phases of the project (i.e., logic, memory, and packaging will be made under one roof) or will serve different purposes (i.e., one building makes logic, another produces memory, yet another does testing and packaging). In any case, when fully built, Terafab will be a massive semiconductor production campus that will require significantly more than $16.8 billion.

The announcement claims that the Terafab facility will employ at least 3,000 people, and that between 60% and 80% of them will be Grimes and nearby Brazos County residents.

Terafab is expected to use water from Gibbons Creek Reservoir instead of local groundwater and feature on-site wastewater treatment as well as water recycling and conservation measures.

The announcement follows Tesla's groundbreaking earlier this year on a research semiconductor facility at the North Campus of Tesla's Giga Texas campus, which the companies describe as a precursor to Terafab.

  •  

Tesla, SpaceX confirm ‘Terafab’ chip fab site — $16.8B first phase

Tesla and SpaceX have confirmed where they’ll build Terafab, the semiconductor megafactory Elon Musk first teased in March. It’s going to Grimes County, Texas, about an hour northwest of Houston.

The companies put the initial phase at roughly $16.8 billion and said the finished site will span more than 100 million square feet, which they’re calling the largest chip manufacturing facility on the planet.

  •  

Shedding light on new type of magnetism in quantum materials

Recently, the field of magnetics has seen the proposal of a new class of magnetism called altermagnetism, which could allow advances in miniaturizing and improving RAM architecture in computers. Rice University's Ming Yi, together with collaborators Bharat Jalan of the University of Minnesota and Milan Radovic of the Paul Scherrer Institute, recently published a paper in Science Advances showing that the quantum material ruthenium dioxide potentially displays this new altermagnetism in its ultrathin-film form, in which the material is prepared as a thin slice only a few atomic layers thick.

  •  

Lumentum CEO warns of impending bottleneck on critical material used for silicon photonics — fab and material shortfall already lags 30% below customer needs as co-packaged optics demand skyrockets

Lumentum CEO Michael Hurlston told an audience at the RAISE Summit in Paris earlier this month that indium phosphide, the compound semiconductor behind every laser in an AI data center, is heading into a supply squeeze worse than what we've already seen with DRAM / NAND, and that Nvidia's decision to fund Lumentum and its biggest competitor at the same time was a response to exactly that.

In his remarks, Hurlston said that telecom customers bought lasers in the hundreds, while Nvidia and the hyperscalers are asking for hundreds of millions. While Lumentum runs five indium phosphide fabs, it's still shipping more than 30% below what customers want. Nvidia's answer, in March, was to write $2 billion checks to Lumentum and Coherent, the two suppliers that, between them, make most of the world's high-speed datacom lasers, with purchase commitments and future capacity access attached to both.

"Between the two of us, I don't think we can service the demand that Nvidia and others are now putting on us to solve this resistance problem in the data center," Hurlston added.

Silicon doesn't emit light

Indium phosphide has a direct bandgap of roughly 1.34 eV, which lets it convert electrical current into photons efficiently. Silicon's bandgap is indirect, so it can guide, split, and modulate light but can't generate it. Every silicon photonics platform in production, including those of Nvidia, Broadcom, Marvell, and Cisco, still needs an indium phosphide laser somewhere in the package to supply the light for silicon to manipulate. Moving from pluggable transceivers to co-packaged optics changes where that laser sits and how it's mounted, but it doesn't remove it from the bill of materials.

Nvidia's marketing claims its photonics switches use four times fewer lasers than an equivalent pluggable deployment, alongside 3.5 times better power efficiency and ten times better network resiliency, all of which are vendor figures. Those savings are per port, and it's that port count that's exploding.

The high-end Spectrum-X Photonics configuration runs 512 ports at 800 Gb/s for 400 Tb/s of switching, and Quantum-X Photonics InfiniBand runs 144 ports at 800 Gb/s. Co-packaging also shifts the laser type toward high-power continuous-wave sources and external laser modules that feed multiple channels, which are harder to build than the electro-absorption modulated lasers inside a conventional pluggable. Coherent's Nvidia agreement covers that category of high-power CW lasers, external laser source modules, and fiber array units.

Capacity at Lumentum and Coherent

Lumentum posted record revenue of $808.4 million in its fiscal third quarter, up 90% year over year, with components revenue of $533 million and pump laser shipments up 80%. On the May earnings call, Hurlston told analysts the company expects its supply line to increase 50% measured from one December quarter to the next, and in the same breath said the supply-demand imbalance on EMLs had widened from the 25% to 30% given a quarter earlier to "somewhere greater than 30%," with pump lasers tighter still. A supplier growing output by half a turn per year and losing ground anyway is a clean measure of how steep the demand curve is.

Coherent's 6-inch indium phosphide line yields more than four times as many devices as its 3-inch line at less than half the cost, CEO Jim Anderson told investors on the company's fiscal Q3 call. Anderson said EMLs, CW lasers, and photodiodes are all in production on the 6-inch line with yields above the legacy 3-inch lines, and that internal capacity would double by the end of the June quarter, one quarter ahead of plan, then more than double again by the end of 2027. Coherent's revenue hit a record $1.8 billion, up 21%, with data center and communications now 75% of the total against roughly 41% a year earlier, and backlog stretching into 2028.

Logic and memory moved to 300mm wafers in the early 2000s. Indium phosphide is a brittle, expensive, small-boule material where the industry-wide upgrade currently underway is 3-inch to 6-inch, roughly the transition silicon completed in the 1980s. Lumentum's fifth fab, announced in March, is a converted Qorvo gallium arsenide plant in Greensboro, North Carolina, described as 4-inch and 6-inch compatible and ramping around 2028.

Running through China

Indium is recovered as a byproduct of zinc refining, so its output can't be scaled independently of zinc economics, no matter how much laser demand there is. The USGS Mineral Commodity Summaries 2026 put China at an estimated 760 tonnes of roughly 1,100 tonnes of global primary refined indium in 2025, about 69%, and recorded a 72% year-over-year fall in unwrought indium exports between September 2024 and September 2025 after Beijing placed the metal under export controls in February last year. The U.S. warehouse price averaged about $390 per kilogram in 2025 against $340 in 2024.

AXT's Chinese subsidiary Tongmei had to obtain Ministry of Commerce export permits, granted in June and August 2025, before it could resume shipping indium phosphide substrates out of China. The fabs Nvidia is funding sit downstream of that licensing regime, and the wafers going into them aren't made in the United States in meaningful volume.

DRAM contract prices rose 90% to 95% quarter over quarter in Q1 2026, the largest quarterly increase TrendForce has recorded, and the firm forecast a further 58% to 63% in Q2 with NAND up 70% to 75%. HBM is sold out for 2026. Hurlston is measuring his warning against a genuinely historic crunch, which makes it a strong claim rather than a throwaway one, and he runs a company whose valuation depends on the shortage persisting.

LightCounting's April 2026 market forecast puts current transceiver demand about 30% above supply, matching Lumentum's own figure, but states that the shortages should be gone by the end of 2026 and cuts expected Ethernet transceiver growth to 65% for the year after 82% in 2025 and 93% in 2024. Coherent, hitting its capacity doubling a quarter early, points the same way. The distinction from memory is that the fix here is a wafer-size transition already running in production with yields ahead of the old node, not a new fab that takes three years to build.

  •  

Shanghai Aishengna named as the maker of China's first domestic immersion DUV chipmaking tools — first viable domestic 7nm-capable scanner to be completed by 2038

Reuters has named Shanghai Aishengna Electronic Technology Group as the state-owned company producing China's first domestic immersion deep ultraviolet lithography (DUV) scanners, a day after news of the program broke without identifying the manufacturer. Aishengna was established in August 2023 with RMB 7 billion, around $1 billion, in registered capital and is thought to have absorbed engineering teams from Shanghai Yuliangsheng Technology and Shanghai Micro Electronics Equipment.

Aishengna has been named by a single source who declined to be named, and its shareholders, SMEE and Yuliangsheng, didn’t respond to requests for comment. SMIC has been testing a Yuliangsheng immersion tool since September 2025, and first deliveries are slated for SMIC, Hua Hong Semiconductor, and ChangXin Memory Technologies.

Photoresist, coater tracks, and light sources

Tokyo Electron held an 89% share of the global coater/developer market in 2022, per Shared Research's analysis of the company's own disclosures, with its chief executive putting the figure near 90% and at 100% for EUV production. A scanner only exposes the wafer, however. It’s the track that's responsible for applying the resist film, baking it, and developing the pattern after exposure, and it has to be mechanically and thermally matched to the scanner in a single cluster, which is why the two are bought together. Shenyang Kingsemi has reached 28nm-class track capability and is currently targeting 14nm.

JSR, Tokyo Ohka Kogyo, Shin-Etsu, and Fujifilm hold a combined 72.5% of the ArF photoresist market, while Chinese suppliers hold under 1% of ArF immersion resist specifically. Nata Opto-electronic built a 25-ton ArF line, later expanded to 50 tons, passed customer qualification in December 2020, and completed project acceptance in 2024 with little volume to show for it. Xuzhou B&C says its ArF immersion products cover 45nm to 28nm and can stretch to 14nm, and chairman Fu Zhiwei has put mass production of China's core advanced resists five years out.

Cymer, Gigaphoton, and Coherent hold more than 80% of the ArF excimer laser market between them, and Cymer has been an ASML subsidiary since 2013. Beijing RSLaser shipped China's first high-power domestic excimer laser in 2018 under the national Project 02 program and has a 4 kHz 193nm ArF prototype aimed at 90nm and 65nm-class tools, generations behind what 28nm immersion requires.

Carl Zeiss SMT has been ASML's sole projection optics supplier since 1983, and Zeiss SMT revenue grew from €1.2 billion in 2016 to €4.1 billion in 2024. It’s not currently known what, if any, Japanese tooling is inside the Aishengna machines, but excimer sources and precision optics are areas where Chinese substitution is believed to be lacking.

CXMT

CXMT is projected to reach around 350,000 wafer starts per month by the end of 2026, roughly 25,000 short of Micron, up from 40,000 in 2020. DRAM scaling at 1a and 1b-class nodes runs on immersion multipatterning because CXMT has no EUV access, which makes any potential ramp lithography-gated rather than cleanroom-gated. DRAM contract prices rose 93% to 98% quarter on quarter in Q1 2026, and TrendForce projected a further 58% to 63% in Q2, lifting DRAM industry revenue 81% to $97 billion. A domestic immersion source is therefore worth having to CXMT, even at inferior overlay and throughput.

A DUV-only 7nm flow needs roughly 19 spacer-defined multipatterning masks from the front end through the second metal layer, against about 10 for an EUV-based N7+ process, by one published comparison of SMIC's process. SemiAnalysis has put SMIC's 7nm defect density near 0.14, around double TSMC's N5 and N6. ASML CEO Christophe Fouquet told analysts during the company's July earnings call that rising DRAM lithography intensity partly reflects "the increased replacement of multi-patterning with more cost-effective single-exposure EUV." As such, every exposure China adds to compensate for the missing EUV burns scanner hours a thin domestic fleet doesn't have.

The MATCH Act

China fell to about 14% of ASML's sales in Q2 2026 from 33% across 2025, and installed base management, the service and upgrade business, brought in €2.8 billion of ASML's €9.3 billion in second-quarter revenue. H.R. 8170 would ban both the export and the servicing of immersion DUV systems to any destination in China and designate SMIC, Hua Hong, Huawei, CXMT, and YMTC as restricted entities by statute. Former ASML chief executive Peter Wennink has said the company can service most Chinese tools, but not with spare parts of U.S. origin that fall under export control, which is the mechanism that the MATCH Act would widen.

The bill remains in committee after clearing the House Foreign Affairs Committee in April, with a Senate companion filed as S. 4281, and no floor vote yet scheduled. Its 150-day allied-alignment clause would also reach Nikon, which sold 11 ArF immersion systems in FY2024 and none in the first three quarters of FY2025, and which plans to deliver a new immersion prototype to a major chipmaker by 2027. ASML expects about 130 immersion shipments this year and intends to raise immersion capacity 30% in 2027, with a further 30% under investigation for 2028.

As for Chinese providers, SMEE prototyped its SSA600 ArF tool in 2011 and never reached sustained commercial sales, and a late-2023 shareholder claim that the company had developed a 28nm machine was subsequently retracted. SiCarrier showed etch, CVD, PVD, and ALD tools at SEMICON China 2025 without a lithography system, and a December 2025 government contract reported as a lithography award turned out to cover a KrF tool at 110nm. We’ve previously assessed that China’s toolmakers are more than a decade behind the market leaders.

The AI Futures Project's June forecast puts a commercially viable domestic 7nm-capable immersion scanner between 2032 and 2038, with a median of 2035, and claims ASML holds 98.7% of the immersion market today. Five machines in 2026 would be under 4% of ASML's annual immersion output, and each would still need a coater track, a qualified ArF immersion resist, and an excimer source to print a single wafer; China leads in none of those three.

  •  

Prototype device polarizes light with heat for denser optical signals

Researchers have found a way to speed up components that control light polarization in optical communication and computing. Polarization is a property of light that can carry additional information along with the primary signal, enabling higher data throughput. State-of-the-art components that control polarization in optical circuits have to be physically rotated many times a second, wasting precious time. Instead, this can be achieved by varying the temperature of the material the light passes through.

  •  

Trump admin secures record $265 billion TSMC investment in U.S. semiconductor manufacturing, adding 4 new facilities for total of 12

TSMC

In a major boost to American domestic manufacturing, the Trump Administration today announced that Taiwan Semiconductor Manufacturing Company (TSMC) is committing an additional $100 billion in investments for advanced semiconductor facilities in the United States. This brings TSMC’s total planned investment to $265 billion — one of the largest foreign direct investments in American history.

The announcement, made jointly by the White House and the Department of Commerce, highlights the success of strategic trade and investment partnerships, particularly the historic U.S.-Taiwan deal signed in January 2026. As a direct result, TSMC will build four additional advanced semiconductor manufacturing and packaging facilities, bringing its U.S. footprint to 12 leading-edge facilities, primarily in Arizona.

Building on Momentum

This latest expansion builds on previous commitments. TSMC’s original plans started at around $65 billion, which were later increased. The new infusion underscores sustained momentum under the current administration’s focus on reshoring critical supply chains.

In a statement, U.S. Commerce Secretary Howard Lutnick emphasized the job-creating impact, “President Trump’s leadership is driving companies to invest in American manufacturing. TSMC’s announcement of an additional $100 billion investment following our historic deal on trade and investment with Taiwan will create tens of thousands of American jobs and bring advanced semiconductor manufacturing back to America.”

TSMC Chairman and CEO Dr. C.C. Wei echoed the sentiment, crediting collaboration with the administration and strong U.S. customer demand, “We appreciate the strong collaboration and support of the Trump Administration, Secretary Lutnick and our leading U.S. customers… This is to support the strong multi-year demand from our leading U.S. customers, and we believe this investment will further foster the development of the U.S. semiconductor ecosystem, strengthen the supply chain, and support significant job creation in the United States.”

Economic and Strategic Impact

The investments are expected to generate significant construction and high-tech jobs, along with billions in indirect economic output. Beyond direct facilities, the broader U.S.-Taiwan trade and investment framework is catalyzing an additional $500 billion in Taiwanese investments — $250 billion in direct semiconductor and related enterprises, plus another $250 billion to strengthen the full supply chain in the U.S.

This move addresses long-standing concerns about reliance on overseas production for advanced chips, especially those critical for AI, defense, automotive, and consumer electronics. By expanding domestic capacity with a world-leading foundry like TSMC, the U.S. strengthens its position in the global semiconductor race while creating high-paying opportunities for American workers.

The Trump Administration’s approach, which combines diplomatic deals, incentives for onshoring, and a focus on national security, continues to yield concrete results in rebuilding America’s industrial base.
‎
MacDailyNews Take: With 12 state-of-the-art facilities on track, America is poised to capture a much larger share of advanced chip production. This not only bolsters economic competitiveness, but also enhances supply chain resilience against geopolitical risks.


‎
Please help support MacDailyNews — and enjoy subscriber-only articles, comments, chat, and more — by subscribing to our Substack: macdailynews.substack.com. Thank you!

Support MacDailyNews at no extra cost to you by using this link to shop at Amazon.

The post Trump admin secures record $265 billion TSMC investment in U.S. semiconductor manufacturing, adding 4 new facilities for total of 12 appeared first on MacDailyNews.

  •  

Harnessing Machine Learning to Solve Complex Inverse Problems in Semiconductor Analysis

In a groundbreaking advancement poised to revolutionize semiconductor analysis, a team of researchers from the Institute of Science Tokyo has pioneered a tandem neural network (TNN) architecture that dramatically accelerates the inference of vital material parameters from transistor measurements. This novel machine learning framework addresses one of the most vexing challenges in semiconductor physics—the multivalued inverse problem—achieving unprecedented speed and accuracy that eclipses traditional computational methods.

Semiconductor devices underpin nearly every aspect of modern electronics, from smartphones to sophisticated computing systems. The performance and reliability of these devices hinge on intricate material properties such as defect densities, trap states, and charge carrier mobilities. While engineers can rapidly measure transistor behavior through current-voltage characteristics, deciphering the precise material attributes driving this behavior remains an elusive inverse problem. Conventional approaches rely heavily on iterative simulations and optimization techniques, often consuming hours or even days to converge on plausible solutions.

At the heart of the difficulty lies the phenomenon of multivaluedness: distinct combinations of semiconductor material parameters can yield virtually indistinguishable transistor responses. This ambiguity complicates the task of tracing device performance back to its physical origins. The research team recognized that conventional simulation frameworks are ill-equipped to navigate this degeneracy efficiently. Their insight was to harness the power of tandem neural networks, an innovative deep learning configuration capable of simultaenously enforcing physical consistency and mathematical plausibility in parameter estimation.

The tandem neural network developed by the team couples two interconnected models operating in series. The initial inverse model proposes candidate sets of material parameters based on observed transistor behavior. This output then feeds into a forward model pre-trained to reconstruct transistor characteristics from material parameters. By integrating the forward model’s reconstructions into the training loss function of the inverse network, the system effectively teaches itself to generate solutions that not only fit the measurement data but also align with the physical laws governing transistor operation.

Training this sophisticated architecture required an extensive dataset of over 1,000 simulated transistor measurements, specifically focusing on amorphous indium-gallium-zinc oxide (a-IGZO) transistors—a material of significant interest for flexible and transparent electronics. The dataset spanned a parameter space roughly 1,000 times broader than previous studies, encompassing six key variables: defect density, electron trap states, and carrier mobility among them. Astonishingly, the TNN inferred all six parameters from a single transistor current-voltage curve in less than one millisecond, achieving near-perfect accuracy across the range.

Beyond simulations, real-world validation was paramount. The researchers fabricated a series of a-IGZO transistors under five distinct processing conditions in their laboratories. When subjected to the TNN analysis, the model reproduced the measured device characteristics with exceptional fidelity, requiring no parameter tuning or iterative refinement. This immediate, high-precision performance marks a quantum leap compared to traditional simulation-dependent approaches that demand repetitive calculations, often spanning hours or days.

Assistant Professor Keisuke Ide, one of the principal investigators, highlighted the transformative implications of this speedup: “Our tandem neural network achieves a computational acceleration exceeding six orders of magnitude relative to conventional device simulation methods. This means what once took days can now be done almost instantaneously, radically changing the landscape of semiconductor diagnostics and research.”

The implications of this advancement extend well beyond academic curiosity. In industrial manufacturing, instantaneous and ultra-accurate assessment of transistor material properties can serve as an integral part of quality control, allowing defects and performance variants to be detected and addressed on the production line in real-time. This rapid feedback loop could markedly reduce waste and improve yield in semiconductor fabrication facilities.

Moreover, the TNN framework paves the way for autonomous laboratories where artificial intelligence designs, executes, and interprets experiments with minimal human oversight. By swiftly and reliably unraveling complex material-property relationships, AI-driven research tools can accelerate innovation cycles, optimizing device designs and material formulations in ways previously unattainable due to computational bottlenecks.

Interestingly, the tandem neural network architecture is not conceptually limited to semiconductors alone. The researchers underscore its potential applicability across a broad spectrum of inverse problems characterized by multivaluedness, spanning materials science, chemistry, optics, and possibly even biological systems where multiple underlying parameter sets may produce indistinguishable observational data.

The Institute of Science Tokyo, newly established in 2024 through the merger of Tokyo Medical and Dental University and Tokyo Institute of Technology, serves as a nexus for such cutting-edge interdisciplinary research. This project exemplifies the institute’s mission to advance scientific understanding and technology in ways that create tangible value for society.

As the demands for faster, smaller, and more efficient semiconductor components intensify, novel computational tools that can disentangle the complex interplay of material parameters swiftly and accurately become indispensable. The tandem neural network approach represents a critical milestone on this journey, ushering in a new era where machine learning not only supplements but fundamentally transforms physical sciences research.

This rise of AI-powered physics inference is poised to fuel accelerated material discovery, optimized manufacturing, and ultimately, enhanced electronic devices that power tomorrow’s technological landscape. With this tandem neural network, researchers have cracked open the door to solving multivalued inverse problems at blistering speeds, a feat that was once considered beyond reach.


Subject of Research: Semiconductor material characterization using machine learning

Article Title: Tandem Neural Network Rapidly Solves Multivalued Inverse Problems: Application to Oxide-Semiconductor Characterization

News Publication Date: 27-May-2026

Web References: https://doi.org/10.1002/aisy.70437

Image Credits: Institute of Science Tokyo

Keywords

Artificial intelligence, machine learning, semiconductor analysis, inverse problems, multivaluedness, twin neural networks, material characterization, oxide semiconductors, transistor diagnostics, amorphous indium-gallium-zinc oxide, computational speedup, autonomous laboratories

  •  

Artificial synapse uses light-color programming for brain-like balanced learning

The human brain actively keeps "learning" in balance by holding on to what matters and letting go of what does not. Researchers in Korea have now reproduced this ability in a semiconductor device, using the color of light to strengthen (remember) or weaken (forget) an artificial synapse's memory. Remarkably, the key ingredient is a material "defect" that engineers usually try to eliminate. The study appears in Nature Communications.

  •  

AI model extracts hidden semiconductor properties from simple transistor tests in under 1 millisecond

A tandem neural network capable of inferring key physical parameters of semiconductor materials from simple transistor measurements has been developed, as reported by researchers from the Institute of Science, Tokyo. While conventional approaches for this type of analysis require hours or even days, the proposed system produces results in under 1 millisecond with near-perfect accuracy.

  •  

Revolutionary High-NA Lithography Optical System Set to Transform Semiconductor Chip Manufacturing

In the rapidly advancing world of semiconductor technology, the relentless pursuit of smaller, faster, and more energy-efficient computer chips is critical to powering the next wave of innovation—from artificial intelligence mega-data centers to cutting-edge medical devices and ubiquitous consumer electronics. At the frontier of this evolution lies extreme ultraviolet (EUV) lithography, a sophisticated method capable of etching circuit patterns at the nanometer scale. However, the intrinsic complexities and astronomical costs associated with current EUV lithographic systems have presented formidable barriers to wider adoption and scalability. Now, a groundbreaking proposal from Professor Tsumoru Shintake of the Okinawa Institute of Science and Technology (OIST) offers a transformative vision for this technology, promising to revolutionize semiconductor manufacturing with unprecedented precision, reduced complexity, and drastically lower costs.

EUV lithography operates by harnessing light with an extraordinarily short wavelength—just 13.5 nanometers—which enables the creation of incredibly fine features on silicon wafers. The process begins when this EUV light is generated and meticulously channeled through an illumination system towards a reflective photomask imprinted with the target circuit design. Upon reflection, this patterned light passes through a projector system composed of precisely curved mirrors, which shrink and focus the intricate design onto a silicon wafer. Subsequent processing etches the illuminated pattern into the wafer’s surface, forming the foundational architecture of semiconductor chips. Crucial to pushing the envelope of miniaturization is the numerical aperture (NA) of these systems—a parameter that defines the range of angles over which the system can accept or emit light. Higher NA values correlate directly to finer resolution capabilities, enabling denser packing of transistors and circuit elements.

Despite the theoretical promise of high-NA EUV lithography, practical implementation has been fraught with challenges. The early explorations into high-NA configurations favored simple in-line setups wherein the photomask, projector, and wafer are aligned along a single optical axis. This streamlined arrangement, while intuitively appealing, introduced significant optical aberrations such as distortions and blurring that intensified with increasing NA. These so-called “mask 3D effects” arise due to the complex interplay of light reflections on the three-dimensional topography of the photomask, adversely affecting pattern fidelity and ultimately the electrical performance of the fabricated chips.

Confronting these longstanding obstacles, Professor Shintake embarked on an ambitious reimagining of the illumination and projection components integral to high-NA EUV lithography. His initial foray involved evaluating the feasibility of a minimalist projector design consisting of a single pair of mirrors—one concave and one convex—with the potential to deliver high-resolution imagery while suppressing aberrations. Although this simplistic approach did not yield immediate success, continued exploration led to a sophisticated two-stage projection configuration. Each stage utilizes a concave-convex mirror pair arranged to optimize optical performance. Remarkably, simulations revealed that carefully orchestrated multiple reflections between these mirrors could cancel out deleterious optical defects, preserving the high numerical aperture without compromising image quality.

These insights emerged from extensive computational modeling conducted using OpTaliX, an advanced optical simulation software. Through meticulous parameter optimization, including mirror curvature adjustments and precise spatial positioning, Shintake and his collaborators delineated an optical path that maintains high resolution while mitigating the distortive mask 3D effects. The theoretical framework underscores the power of optical engineering in overcoming fundamental diffraction and interference phenomena—challenges that have hampered high-NA EUV lithography efforts for decades.

Beyond the technical elegance of the design, the proposed system carries profound economic implications. Current state-of-the-art EUV lithography machines reportedly cost hundreds of millions of euros each, placing them out of reach for all but the largest semiconductor manufacturers. In stark contrast, Shintake’s approach promises to slash these costs dramatically—potentially to just a quarter of today’s expenditures—thus democratizing access to cutting-edge lithography and accelerating development cycles across the industry.

The ramifications extend well beyond chip manufacturing economics. The International Energy Agency forecasts that by 2030, global data center electricity consumption will double, driven largely by the proliferation of energy-intensive artificial intelligence applications. Higher-density chips fabricated with the new high-NA technology would feature electronic pathways shortened by virtue of their finer architectural detail, reducing signal travel distance and thereby minimizing energy loss during computation. Moreover, lower heat emission from these denser chips implies diminished cooling requirements, collectively resulting in meaningful reductions in power consumption and operational costs for data centers worldwide.

As part of his next research phase, Professor Shintake and his team aim to transition from simulation to realization by constructing a physical prototype of the novel high-NA EUV lithography system. This endeavor will necessitate overcoming engineering challenges such as fabricating mirrors with near-perfect reflectivity and minimal surface defects—criteria assumed in simulations but challenging to achieve in practice. Nonetheless, the initial groundwork laid by this study establishes a compelling blueprint for transforming semiconductor fabrication.

In addition to enabling finer patterning capabilities, the simplified in-line projector design enhances overall system robustness and manufacturability. By aligning the photomask, projector, and wafer along a single axis with optimized mirror pairs, the architecture reduces alignment complexities and optical component counts, thereby facilitating easier maintenance and potentially accelerating throughput rates on the manufacturing floor.

Innovations like Shintake’s not only refresh the physics of lithographic imaging but may also catalyze novel computing paradigms by significantly pushing the achievable limits of miniaturization. As industry demand for memory density and logic efficiency mounts exponentially, high-NA EUV lithography could unlock pathways to next-generation chip designs exhibiting superior speed, reduced energy consumption, and lower production costs, collectively powering advancements in artificial intelligence, quantum computing, and ubiquitous digital technologies.

Ultimately, this research signals a pivotal juncture for semiconductor manufacturing, harnessing the power of optical science to surmount entrenched technical and financial hurdles. By reducing the cost and complexity of high-NA EUV lithography, Professor Shintake’s innovation promises transformative impacts on the silicon industry and beyond—enabling faster, greener, and more affordable electronics that will underpin the data-centric future of society.


Subject of Research: High numerical aperture (high-NA) extreme ultraviolet (EUV) lithography systems for semiconductor chip manufacturing

Article Title: High-NA in-line projector for EUV lithography

News Publication Date: June 12, 2026

Web References: http://dx.doi.org/10.1117/1.JMM.25.2.023801

Image Credits: Andrew Scott, Okinawa Institute of Science and Technology (OIST)

  •  

Broadband Photodetection via Si3N4/n-Si Interface

In a groundbreaking advancement for optoelectronic technology, researchers have unveiled a novel approach harnessing the unique properties of Si₃N₄/n-Si hybrid devices to achieve interface-controlled broadband photodetection. This development promises to revolutionize the efficiency and spectral range of photodetectors, devices integral to a wide array of applications from telecommunications to environmental monitoring. The study, recently published in Scientific Reports, highlights how meticulous control over material interfaces can dramatically enhance device performance, marking a significant leap forward in photodetector design and fabrication.

Photodetectors serve as the eyes of modern electronic systems, converting light into electrical signals that enable everything from digital imaging to fiber optic communication. Traditional photodetectors, however, have long been limited by narrow operational bandwidths and sensitivity constraints, curbing their effectiveness in emerging high-performance applications. By integrating silicon nitride (Si₃N₄) with n-type silicon (n-Si), the researchers have engineered a hybrid platform that deftly overcomes these limitations, exploiting interface phenomena to extend detection capabilities across a broad spectrum of electromagnetic radiation.

At the heart of this innovation lies the strategic manipulation of the Si₃N₄/n-Si interface. Silicon nitride, known for its excellent dielectric properties and chemical stability, acts as both a passivation layer and an optical modulator when interfaced with silicon. This interplay at the atomic and electronic scale shapes charge carrier dynamics, reduces surface recombination losses, and enhances photon absorption efficiency. Such interface engineering ensures that the hybrid device is not only highly sensitive but also capable of operating seamlessly over a wide range of wavelengths, from ultraviolet through visible to near-infrared.

The research team deployed advanced fabrication techniques to precisely control the deposition and interface formation of Si₃N₄ on the n-Si substrate. Utilizing plasma-enhanced chemical vapor deposition (PECVD), they achieved a uniform and defect-minimized nitride layer that adheres perfectly to the silicon surface. This meticulous fabrication step is essential as interface traps, commonly induced by imperfections, can severely degrade photodetector responsiveness and noise levels. By minimizing such imperfections, the hybrid device attains an unprecedented signal-to-noise ratio crucial for sensitive detection tasks.

Optical characterization of the Si₃N₄/n-Si hybrids revealed remarkable broadband responsivity, a parameter quantifying the device’s ability to convert incoming photons across various wavelengths into electric current. The devices demonstrated enhanced photoresponse not only in the visible spectrum but also extended into ultraviolet and infrared regions, surpassing conventional silicon-based photodetectors limited by the bandgap constraints of pure silicon. This broadband sensitivity opens the door to new applications where multispectral light detection is necessary without the need for separate sensors.

One of the pivotal mechanisms for this extended response is the formation of interfacial states that facilitate charge transfer and broaden the spectral detection range. These states effectively lower the energy barriers that typically restrict silicon’s photoresponse, enabling efficient utilization of photons with energies both above and below the traditional silicon bandgap. This effect is modulated by the thickness and stoichiometric composition of the Si₃N₄ layer, parameters finely tuned during device fabrication to optimize performance.

Beyond spectral coverage, the temporal response of these hybrid photodetectors is equally impressive. The devices exhibited fast switching times and low dark currents, essential characteristics for high-speed communications and low-light detection scenarios. Reduced dark current, a measure of unwanted noise in the absence of illumination, directly correlates with enhanced sensitivity, thereby allowing the detection of weak optical signals with unprecedented clarity.

Integration compatibility is another striking advantage of the Si₃N₄/n-Si system. Both materials are well-established in mainstream semiconductor manufacturing, meaning that this innovation can be seamlessly incorporated into existing silicon-based electronic platforms. This compatibility facilitates scaling production while maintaining cost efficiency, a critical factor for commercial adoption in industries such as consumer electronics, healthcare diagnostics, and environmental sensing.

The research also delves into the underlying physics governing the device operation. Through combined experimental and theoretical analyses, the study elucidates charge carrier transport across the interface, the role of interface dipoles, and modulation of the built-in electric field that directs photogenerated carriers. Such detailed understanding offers a roadmap for further improvements, potentially inspiring future hybrid systems with tailored optoelectronic properties suitable for specific industrial applications.

In terms of real-world application, these hybrid photodetectors could significantly enhance the performance of cameras, optical coherence tomography devices, and remote sensing instruments. The broadband detection capability reduces the reliance on multiple sensors, simplifying device architectures and improving reliability. Additionally, their fast response times and stability under various environmental conditions are promising for deployment in harsh or variable environments, including space exploration and autonomous vehicle navigation.

This research marks a notable shift in photodetector technology by emphasizing interface engineering to transcend inherent material limitations. By capitalizing on the complementary properties of Si₃N₄ and n-Si junctions, the study injects fresh momentum into the pursuit of universal photodetectors that excel in speed, sensitivity, and spectral range. The findings underscore the vast potential lying in hybrid material systems, motivating continued exploration into interface-controlled photonic devices.

Looking forward, the researchers suggest exploring further modifications to the Si₃N₄ layer such as doping or introducing nanoscale structuring to tailor the interface behavior. Such advancements may unlock new functionalities like polarization sensitivity or even tunable wavelength selectivity, pushing hybrid photodetectors beyond current performance frontiers. These directions align with the broader scientific quest to develop smarter, more adaptable optoelectronic components for the next generation of information and sensing technologies.

In conclusion, the Si₃N₄/n-Si hybrid photodetector described in this study represents a pivotal development that combines material science innovation with practical engineering to address longstanding challenges in photodetection. Its broadband capability, operational stability, and integration potential poise it as a top candidate for a wide spectrum of applications demanding fast, efficient, and reliable light detection. As industries continue to demand more from photonic devices, such interface-controlled systems stand out as a transformative solution poised to redefine the future of photodetection technology.


Subject of Research: Interface-controlled broadband photodetection in Si₃N₄/n-Si hybrid devices

Article Title: Interface-controlled broadband photodetection in Si₃N₄/n-Si hybrid devices

Article References:
Manfo, T.A., Yıldız, D.E., Bağcı, C. et al. Interface-controlled broadband photodetection in Si₃N₄/n-Si hybrid devices. Sci Rep (2026). https://doi.org/10.1038/s41598-026-57951-y

Image Credits: AI Generated

  •  

Liquid cooling technology for semiconductor chips is 10 times more efficient than previous record

AI data centers are power-hungry. Not only do artificial intelligence computations consume enormous amounts of electricity, but a significant amount of energy is also required to cool the semiconductor chips that heat up during operation. As AI chips continue to deliver higher performance, the amount of heat they generate increases rapidly. As a result, conventional air cooling and external copper heat spreaders are approaching their practical limits. To address this challenge, a KAIST research team has developed an ultra-high-efficiency liquid-cooling technology that cools semiconductor chips from within.

  •  

Nanoengineered wood sets new record for transformer insulation

The world's power grid is straining under the surge in electricity demand from data centers, electric vehicles and renewable energy. And a century-old technology, the power transformer, must support this dramatic increase. A particularly weak link in this is the potential for insulation breakdown, the most frequent indicator of power transformer failures.

  •  
❌